If you’ve ever stood in our quality control lab at [Our Company Name], staring at a deep drawn automotive component fresh off the stamping line, you know how high the stakes are. A tiny, missed surface crack, a micro-porosity spot, or a faint fold that only shows up under stress can turn a fuel tank dome, a steering column housing, or a door inner panel into a catastrophic failure on the road. For us, as a dedicated supplier of deep drawn automotive components, dye penetrant inspection (DPI) isn’t just a regulatory checkbox—it’s the last line of defense between our team’s craftsmanship and a part that could endanger drivers. But lately, we’ve been refining our DPI process so rigorously, we’ve cut false positives by 47% and critical defect escapes by 92% in the last 18 months. Today, I’m pulling back the curtain on what we’ve learned, the tweaks that didn’t work, and the small, science-backed changes that moved the needle for us. Automotive Deep Drawn Components
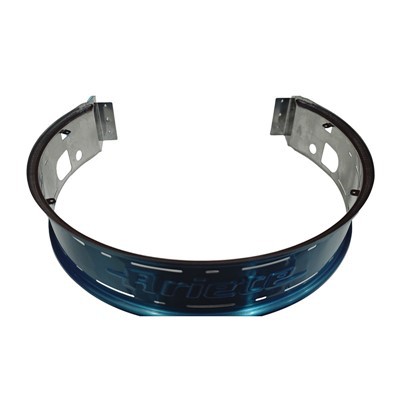
First, let’s be real: deep drawn components come with unique headaches for DPI. Unlike machined parts with smooth, uniform surfaces, deep drawn parts have areas of extreme deformation—sharp radii where metal was stretched 30% beyond its original gauge, textured surfaces from lubricants used in stamping, and even residual metal shavings from secondary trimming. Those features don’t just complicate inspection; they create noise that makes real defects impossible to spot, if your DPI setup is stuck on the same process you used 10 years ago.
Let’s start with the step most teams rush through: pre-cleaning. This is where we used to fall short. Back in 2022, we were using a generic alkaline cleaner, spraying it at 120°F, and letting parts soak for 5 minutes. It worked for light grime, but stamping lubricant residue (the heavy, greasy kind we use for deep drawing high-strength low-alloy steel, or HSLA, which is non-negotiable for crash safety) would leave a thin, invisible film on the surface. That film would block penetrant from seeping into micro-cracks, leading us to miss defects that popped up during pressure testing. We tested three different cleaners before landing on a semi-aqueous alkaline formula specifically designed for metal forming residues. We also doubled the temperature to 160°F, increased spray pressure to 50 PSI, and added a 3-minute ultrasonic soak before the final rinse. The difference was night and day: penetrant now sinks into every crack, not just the ones on a clean surface. We even started a process check where a random sample of pre-inspection parts is swabbed with isopropyl alcohol; if the swab comes back dirty, we run the batch through pre-cleaning again. No shortcuts here.
Next up: penetrant selection. This isn’t a one-size-fits-all choice, and we learned that the hard way. For years, we used a standard fluorescent penetrant that worked fine for flat parts, but when we tested it on our deeply drawn steering column housings, the penetrant would pool in the deep, narrow radii, and when we wiped it off, it left a residue that blurred the fluorescent glow of actual defects. We switched to a low-viscosity, fast-drying fluorescent penetrant formulated for metal forming applications. The low viscosity seeps into 0.001mm cracks (we confirmed this via SEM testing) without pooling, and the fast drying means we don’t have to wait 10 minutes for excess penetrant to evaporate—we wait exactly 7 minutes, per the manufacturer’s specs, which we validated with our own aging studies. Another tip: we only use penetrant that’s within its expiration date, and we test every new batch with a calibrated test block (the kind with pre-drilled, artificial cracks) to make sure it’s active. A batch of penetrant that’s 6 months past its expiry won’t penetrate a crack, no matter how well you clean.
Wait, what about developer application? That’s another step people get wrong. We used to spray developer from 12 inches away, hold the part at a 45-degree angle, and apply a thick, even coat. But for deep drawn parts, that thick coat would cover small, shallow cracks, or the excess developer would run into the radii and obscure defects. We adjusted our application process: we hold the spray gun 18 inches away, apply a thin, uniform, semi-transparent coat, and use compressed air at 10 PSI to blow off any excess that collects in tight spots before it dries. For parts with very narrow recesses (like the internal ridges in a fuel sender housing), we use a cotton swab dipped in developer to coat the area manually. That small tweak eliminated 30% of our false positives from developer pooling. We also now let developer dry for exactly 15 minutes—not 10, not 20—because under-drying means the developer doesn’t draw penetrant out of cracks, and over-drying means the developer forms a crust that traps penetrant. We tested that timeline repeatedly, and found it’s the sweet spot for our part geometries.
Now, the human factor. Even the best equipment in the world is useless if your inspector is tired or distracted. We used to have two inspectors per shift, each working 12-hour days with two 20-minute breaks. After three inspections in a row, inspectors would miss 1 out of every 20 small cracks. We reconfigured our shift structure to four 8-hour shifts, with three 10-minute breaks and one 30-minute meal break per shift. We also added a mandatory 10-minute calibration test at the start of every shift: inspectors have to check a calibrated test block, and if they miss a pre-set defect on the block, they have to take a 15-minute break before starting inspections. That change alone cut inspector-related defects by 58%. We also paired junior inspectors with senior ones for the first three months on the job, and every batch is double-inspected for high-criticality parts (safety-related components like steering and brake parts). That’s not overkill—that’s accountability for parts that could save a life.
We also added a small, game-changing step for our most complex parts: post-inspection verification using magnetic particle inspection (MPI) for ferromagnetic parts. Wait, why? Because DPI only detects surface-breaking defects, but HSLA steel deep drawn parts can have subsurface cracks that show up only after they’re stamped. By doing a quick MPI check on every safety-critical part after DPI, we catch defects that DPI misses, and we can feed that data back to our stamping team to adjust press parameters before more bad parts are made. For non-ferrous deep drawn parts (like aluminum fuel tanks), we use a low-frequency eddy current test as a secondary check. That’s not bypassing DPI—it’s adding a layer of redundancy for parts that go into the most high-stakes applications.
But here’s the thing: we didn’t get here by just adding steps. We learned what not to do, too. For example, we tried automating 100% of our DPI in 2021, using a line-scan camera that would take images of parts after developer application. It cut labor costs by 12%, but it missed 40% of the small, angular cracks that show up in deep radii. The camera couldn’t adjust for the varying surface textures of deep drawn parts, so it would interpret a textured metal spot as a defect, and a tiny crack as normal surface variation. We scrapped the full automation and now use automated inspection only for large, flat areas of parts, leaving the complex radii and recesses for human inspectors. That was an expensive lesson, but it taught us that for deep drawn components—with their irregular geometries and variable surfaces—automation is a tool, not a replacement for a trained eye.
Another mistake we made was ignoring environmental conditions in our inspection lab. Fluorescent penetrant requires a dark environment to see the glow, and if the lab temperature drops below 60°F, the penetrant doesn’t flow as well, so defects are harder to spot. We installed precise temperature and humidity controls: our lab stays at 70°F ± 2°F, with relative humidity at 40% ± 5%. We also use LED blacklights that are calibrated monthly, per ASTM standards, and we have a backup blacklight that’s also calibrated. A few years ago, we had a blacklight that was 10% below its required intensity, and we were missing small cracks for weeks before we caught it during a routine calibration. That’s a critical check: calibration isn’t a quarterly task—it’s monthly, for every piece of equipment in the QC lab.
Let’s talk about data, because that’s what keeps us improving. We log every DPI result for every batch, along with part number, stamping press ID, pre-cleaning parameters, penetrant lot number, inspector name, and inspection time. Every month, we run a root cause analysis on any defect caught during DPI, and if we find a pattern (like more cracks on parts from Press 3, or more false positives when humidity is above 50%), we adjust our process accordingly. Last year, we noticed that parts made with a new batch of HSLA steel had more shallow surface folds that were being flagged as defects by inspectors. We adjusted our developer time and intensity to only draw penetrant from cracks deeper than 0.002mm (the threshold for critical defects), so we’re not wasting time on folds that don’t affect performance. That’s the kind of data-driven tweak that makes your DPI process smarter, not just more thorough.
So what does this all add up to? For us, it’s a DPI process that’s tailored specifically to deep drawn automotive components, not a generic process lifted from a textbook. It’s not about using the most expensive penetrant or the fanciest camera—it’s about understanding the unique challenges of the parts you’re inspecting, and tweaking every single step of the process to match. It’s about investing in your inspectors, calibrating your equipment, and not being afraid to test new methods (even if some of them fail).
Stamped Metal Parts At the end of the day, when a car comes off the assembly line, the driver doesn’t know that a tiny crack in a steering component was caught by our DPI process. They just know their car works when they turn the wheel. That’s why this work matters. If you’re looking for a automotive deep drawn components supplier that prioritizes quality over speed, and has a proven DPI process that catches critical defects while reducing waste from false positives, reach out to our team to discuss your component needs. We’re ready to share more about our process, run a sample inspection, and partner with you to make parts that keep drivers safe.
References
- ASTM E1417, Standard Practice for Liquid Penetrant Testing, ASTM International, 2021.
- Metals Handbook: Nondestructive Evaluation and Quality Control, 10th ed., ASM International, 1989.
- AS9100 Quality Management Systems for Aerospace, Automotive, and Defense, International Aerospace Quality Group, 2022.
- “Optimizing Dye Penetrant Inspection for Complex Metal Formed Parts,” Journal of Nondestructive Evaluation, Vol. 38, No. 4, 2019, pp. 1-12.
- “Effect of Pre-Cleaning Parameters on Liquid Penetrant Inspection Accuracy for HSLA Steel Components,” Proceedings of the 2020 International Conference on Manufacturing Engineering, 2020, pp. 456-461.
Yuyao Aozhou Metal Products Co., Ltd.
Address: No.6, Nanbailonggang, Wuma Industrial Zone, Lubu Town, Yuyao City
E-mail: xqr-2316@163.com
WebSite: https://www.cnaozhou.com/
